- All
- Product Name
- Product Keyword
- Product Model
- Product Summary
- Product Description
- Multi Field Search
Views: 0 Author: Site Editor Publish Time: 2026-09-11 Origin: Site


There is nothing quite as frustrating as suddenly busting your knuckles against a hard metal surface. Knuckle injuries, rounded fastener heads, and ruined project timelines frequently stem from one common culprit in the workshop. That culprit is a tool losing its grip right when you apply heavy torque. However, slipping is rarely just a random accident on the job. Instead, it is a highly predictable failure. It almost always comes down to improper technique, degraded tool integrity, or poor manufacturing tolerances right out of the box.
Understanding these underlying factors can save you significant frustration. In this guide, we will break down the exact mechanical reasons why this dangerous slippage occurs. You will learn industry-standard safe usage protocols to protect your hands and your hardware. Finally, we will provide clear evaluation criteria to help you decide when you should finally replace or upgrade your primary hand tools.
Directional Force Matters: Over 50% of slipping incidents result from applying torque against the weaker movable jaw rather than the fixed jaw.
Tolerance is Critical: "Jaw slop" or play in the worm gear is the primary mechanical cause of a wrench rounding off a nut.
Right Tool, Right Job: Upgrading to a heavy duty adjustable wrench or utilizing specialized jaw profiles can eliminate deflection under high torque.
Hard Limits: Adjustable wrenches are not intended for seized or over-torqued bolts; recognizing this boundary prevents tool damage and injury.
Understanding the physics behind tool slippage is your first step toward preventing it. Unlike fixed box-end wrenches, adjustable designs rely on moving parts to function. Moving parts naturally introduce micro-gaps between components. These tiny gaps often dictate whether your tool grips securely or fails under pressure. When you apply rotational force, you magnify every mechanical weakness hidden inside the tool head.
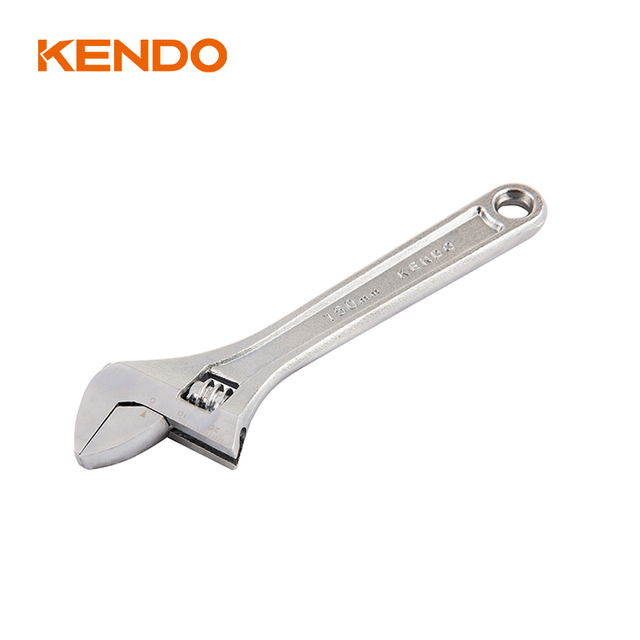
Excessive machining tolerances create a primary point of failure. The knurl, commonly known as the worm gear, controls the opening width. If manufacturers leave excessive play in the knurl's threading, the movable jaw will back off slightly when you apply torque. This tiny shift changes the wrench size mid-turn. You might set the tool perfectly, but the mechanical slop allows it to open up by a fraction of a millimeter during the stroke.
Jaw deflection represents another major mechanical flaw. Inferior metals flex under heavy loads. When the internal track bends, the two jaws no longer sit perfectly parallel to one another. The contact points immediately shift. They move away from the strong, flat sides of the nut and slide toward its vulnerable corners. Once the jaws grip only the corners, severe metal deformation occurs.
You can identify these warning signs before disaster strikes. Keep an eye out for visible gaps between the nut and the jaw while applying light tension. A tool is likely compromised if the worm gear spins freely without immediately engaging the sliding track. Recognizing these observable signs of tool failure allows you to discard a bad wrench before it destroys an important fastener.

Before throwing away a frustrating tool, you must separate user error from actual hardware failure. Many professionals and DIY enthusiasts blame their equipment for mistakes rooted in poor technique. Evaluating your own physical approach is a critical step. If you correct your form and the tool still fails, you can confidently justify purchasing a replacement.
The industry-standard safety rule is clear. You must always pull the handle so the majority of the rotational force transfers directly into the thicker, fixed jaw. The fixed jaw is forged as one continuous piece of steel extending down into the handle. It can withstand immense pressure. Pulling toward the movable jaw stresses the internal gear. Ultimately, this improper technique leads to immediate adjustable wrench slipping.
Pre-torque seating is another essential technique. Many people set the approximate size, slide the tool onto the fastener, and instantly pull. This is a severe mistake. You must outline a new habit. Tighten the worm gear specifically after you place the jaws over the nut. Rolling the knurl tight while the tool sits on the fastener ensures a zero-clearance fit before any force is applied.
Assessing fastener health also dictates your approach. You must inspect the nut before applying any torque at all. An already-rounded or heavily rusted nut requires an entirely different extraction approach. You cannot just tighten the jaws further and hope for the best. Heavily oxidized hardware demands penetrants, locking pliers, or specialized extraction sockets to prevent sudden, violent slippage.
Sometimes your technique is flawless, but the hardware still fails you. This transition point calls for serious hardware evaluation. If you follow the directional pull rule and properly seat the jaws, yet slipping persists, the tool itself is the bottleneck. Continuing to use a compromised wrench will only result in damaged materials and potential physical injuries.
Material quality and forging standards define tool reliability. Standard carbon steel models are cheap, but they warp under intense strain. You should actively seek out drop-forged, heat-treated alloy steel. These advanced metallurgical processes align the internal grain of the steel. As a result, the tool forcefully resists jaw splay even during maximum-effort pulls.
You must perform a features-to-outcomes evaluation when browsing upgrades. Modern tool engineering offers distinct advantages over vintage designs. Consider these specific features:
Hex-Jaw Design: Look for models specifically cut to contact four sides of a hex nut rather than just two. This extra surface area dramatically reduces localized pressure on the fastener corners.
Precision Worm Gears: Evaluate the thread engagement closely. Higher-end wrenches utilize tighter threading. This precision machining reduces the likelihood of the gear backing off under heavy vibration or load.
Laser-Etched Scales: High-quality tools feature clear metric and imperial markings. They allow you to pre-set the approximate size quickly before performing your final zero-clearance tightening.
Upgrading to a heavy duty adjustable wrench resolves these bottlenecks effectively. It also provides significant returns from a business perspective. Investing in premium gear drastically reduces the hidden costs of replacing rounded hardware. It also prevents the massive drain of lost labor time spent extracting stripped bolts.
Professionals frequently face scalability issues when tackling plumbing fittings or large mechanical nuts. A common error involves grabbing a massively long standard wrench simply to achieve the required jaw width. Large diameter fasteners often require delicate handling, not maximum brute force. Using the wrong tool geometry here causes severe component damage.
Applying a massive tool introduces the leverage trap. Picture using a 15-inch standard wrench on a large, delicate brass fitting. The extreme handle length provides a massive mechanical advantage. You will apply far too much leverage without even realizing it. This excessive force risks catastrophic thread damage, cracked pipe unions, or sudden tool slippage.
You need specific engineering for this exact scenario. Introduce the extra wide opening adjustable wrench as the correct evaluation choice. These specialized tools offer massive jaw capacities built into much shorter handles. They come in stubby or standard lengths. They excel in large-diameter, low-torque applications like tightening PVC unions, hydraulic lines, or thin brass fittings.
Shortlisting the right tool requires matching logic. You must guide your purchasing decisions by matching the handle length directly to the actual torque requirement. Simultaneously, match the jaw capacity to the fastener size. Never default to simply grabbing the largest wrench in the box. A targeted approach preserves your delicate hardware while ensuring a snug, non-slip grip.
Implementation risks apply to every piece of equipment you own. Even premium, high-tolerance tools will fail rapidly if not properly maintained. Dirt, metal shavings, and debris love to settle inside the worm gear. Once trapped, this grit mimics the symptoms of poor machining tolerances. It grinds against the internal track and prevents the jaws from locking tightly.
Cleaning and lubrication dictate the lifespan of your equipment. You must clean the sliding track regularly. Use safe cleaning agents to strip away old, contaminated grease. Once clean, you should apply dry lubricants. PTFE or dry graphite sprays work best. They keep the worm gear operating smoothly without attracting abrasive airborne grit.
Malfunction Symptom | Mechanical Cause | Recommended Solution |
|---|---|---|
Knurl is difficult to turn | Trapped grit or heavy rust inside the worm gear | Apply degreaser, scrub with a wire brush, and lubricate with dry PTFE. |
Movable jaw drifts open during use | Worn threads on the knurl or track | Keep your thumb firmly on the knurl while turning. Consider tool replacement. |
Jaws only grip the corners of the nut | Jaw deflection from low-quality steel forging | Upgrade to drop-forged alloy steel for better rigidity. |
Establishing an inspection routine protects you from unexpected failures. You should frequently perform the "Wiggle Test" to assess your current inventory.
Close the wrench jaws completely until they touch.
Pinch the movable jaw between your thumb and index finger.
Attempt to slide the jaw back and forth along the track without turning the knurl.
Attempt to rock the jaw side to side.
If the movable jaw wiggles more than a specified fraction of a millimeter (usually about 0.5mm), the internal tolerances are shot. The tool can no longer guarantee parallel alignment under load. You should downgrade it strictly to light-duty use or discard it entirely.
Protecting your hands and your hardware requires a balanced approach. You must combine correct operational technique with high-tolerance equipment. Always remember to pull the handle toward the solid, fixed jaw. Pre-seat the jaws tightly against the fastener before applying force.
We must also reinforce realistic expectations. Adjustable tools provide incredible versatility, but they possess strict operational limits. They cannot replace dedicated socket sets for seized or specialized high-torque applications. Recognizing these boundaries is the mark of an experienced professional.
Take action today by auditing your current toolbox. Run the simple wiggle test on your most-used wrenches. Consider upgrading your everyday carry to heavy-duty, tight-tolerance models. A small upgrade today protects your vulnerable fasteners, prevents frustrating project delays, and keeps your knuckles safely intact.
A: Vibration and loose worm gear tolerances cause the knurl to spin backward. This mechanical slop allows the movable jaw to drift open. To prevent this, actively keep your thumb pressed firmly against the knurl while applying rotational force.
A: Yes. When the tool slips, it crushes and rounds off the vulnerable corners of the fastener. This strips away the hexagonal shape entirely. Once rounded, it becomes nearly impossible to remove the bolt safely, even if you switch to the correct fixed box-end wrench later.
A: You must always pull. Pulling guarantees mechanical control. Pushing forces you to throw your body weight forward. If the fastener breaks loose or the tool slips off suddenly, pushing removes your ability to catch yourself, often leading to severe hand injuries against sharp surfaces.
A: You should switch to a socket whenever a fastener is severely rusted or seized. Sockets are also mandatory when you require high breakaway torque or when you are doing final-pass torquing to meet a specific, tightly regulated manufacturer specification.